Clad plates are welded in two stages: first the base metal (usually carbon steel) with a matching carbon-steel filler, then the clad side with an alloy filler that restores full corrosion resistance — often with a buffer layer in between. The key rule is to keep base-metal filler out of the clad layer, because diluting the alloy destroys its corrosion resistance. Reactive metals such as titanium cannot be welded to steel at all and are joined with cover strips instead.
1. Cutting and edge preparation
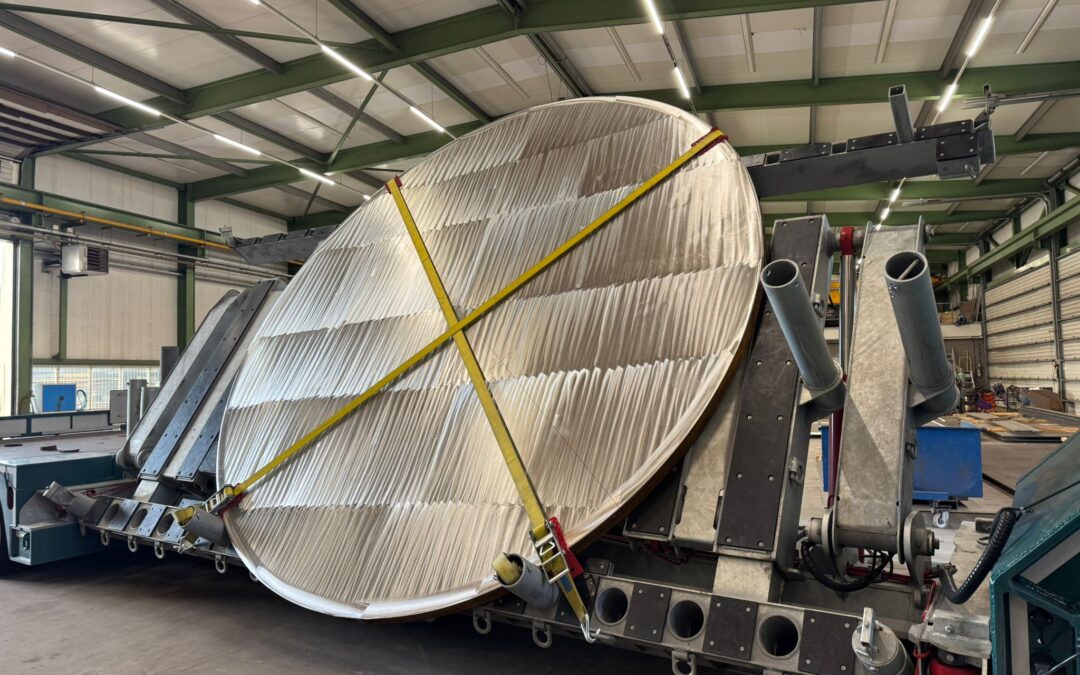
- Cut by plasma, waterjet or machining. Shockwave can supply clad plates waterjet-cut to shape on its 10 × 4 m table.
- Choose a joint design that lets you weld the base from the base side first, for example a V- or X-groove with the root on the base side.
- Remove a narrow strip of clad (cut-back) near the root where the base-metal weld would otherwise melt into it.
- Clean the clad side carefully: no carbon-steel grinding discs or brushes on stainless or nickel alloys.
2. Weld the base metal first
Weld the carbon-steel base with a carbon-steel filler and a procedure qualified for the base material. Do not let the carbon-steel weld reach into the clad layer: iron pick-up would cause cracking and lower the corrosion resistance of the alloy side.
3. Weld the clad side
Over the base weld, deposit a buffer (transition) layer with an over-alloyed filler, then cap with a filler matching the clad layer. Typical choices:
| Clad layer | Buffer layer | Cap layers |
|---|---|---|
| 304L / 316L stainless steel | 309L / 309LMo | 308L / 316L |
| Duplex 2205 | 309L or duplex filler | 2209 |
| Nickel alloys (625, 825, C-276) | Nickel-alloy filler (e.g. ERNiCrMo-3) | Filler matching the clad alloy |
| Copper-nickel | Nickel or CuNi 70/30 filler | CuNi filler |
| Titanium, zirconium | Not fusion-weldable to steel — use cover strips (below) | — |
Fillers are examples; always follow the clad manufacturer’s data and a qualified welding procedure (WPS/PQR per ASME IX or ISO 15614).
4. Titanium-clad and other reactive metals
Titanium and steel form brittle intermetallics, so the titanium layer is cut back from the joint, the steel is welded, and the gap is covered with a titanium cover (batten) strip fillet-welded only to the titanium clad under full argon shielding. Small tell-tale holes in the steel let you leak-test the space underneath. See titanium clad plate.
5. Heat treatment and testing
- PWHT: follow the code for the base material. The explosion bond withstands normal post-weld heat treatment — Shockwave re-tests bond specimens after simulated PWHT cycles (e.g. 620 °C for 60–180 minutes).
- Testing: ultrasonic testing of the bond next to the weld, dye penetrant on the clad-side weld, and ferrite or PMI checks on stainless and nickel-alloy welds.
More about clad plates, what a clad plate is and dissimilar metal welding.
Frequently asked questions
How do you weld clad plate?
Weld the carbon-steel base first with carbon-steel filler, keeping it out of the clad layer. Then deposit a buffer layer with an over-alloyed filler and cap the clad side with filler matching the clad alloy.
What filler is used for stainless clad plate?
Typically 309L or 309LMo as the buffer layer over the carbon steel, followed by 308L or 316L to match the stainless clad.
Can titanium clad plate be welded?
The titanium cannot be fusion-welded to the steel. The clad is cut back, the steel is welded, and a titanium cover strip is welded over the joint to the titanium clad only.
Does the explosion bond survive post-weld heat treatment?
Yes. Shockwave tests bond specimens after simulated PWHT cycles, for example 620 °C for 60–180 minutes, to prove the bond survives fabrication.
Why weld the base metal first?
So that iron from the carbon-steel weld does not dilute the clad layer, which would reduce its corrosion resistance and can cause cracking.
Written by Joeri Hofstede, CEO of Shockwave Metalworking Technologies — vacuum explosion welding specialists since 1985.